Packaging for medical devices and accessories is critical to clinical safety and treatment outcomes. Implantable devices, surgical instruments, and diagnostic reagent components require packaging solutions that meet rigorous standards for cleanliness, sterility and sealing performance. Conventional industrial packaging fails to comply with healthcare industry regulations, making specialized medical-grade packaging a core focus for medical manufacturing development.
Based in-depth research on healthcare industry requirements,Star Group has launched high-standard medical-grade nylon vacuum bags. Manufactured with brand-new medical-grade raw materials in standardized clean-room environments, the bags feature high barrier performance, excellent puncture resistance, stable sealing capability, and compatibility with ethylene oxide sterilization processes. Unlike ordinary industrial packaging bags, medical-grade nylon bags eliminate impurities and contamination risks, enabling reliable sterile sealing and moisture protection for surgical instrument parts, implantable components and medical consumables.
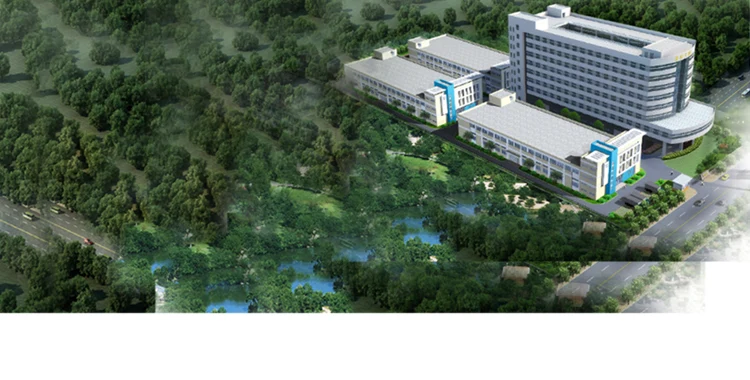
The consistent quality of Star’s medical-grade packaging is supported by substantial hardware investment. The group operates a modern manufacturing base of over 200,000 square meters, including thousands of square meters of professional clean production areas. Strict full-process quality control is implemented throughout production, with rigorous inspections covering raw material selection to finished product delivery. For medical enterprises, partnering with Star means accessing compliant, customizable manufacturing capabilities and high-quality medical packaging solutions tailored to diverse industry needs.