Technical Analysis of Aluminum-Plastic Heavy-Duty Bags: How Multi-Layer Composite Structures Serve High-End Industrial Packaging
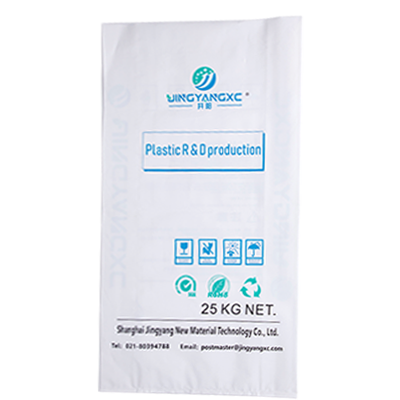
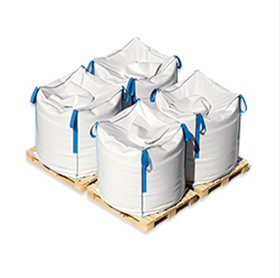
In industries such as chemical, electronics and pharmaceuticals, 25kg heavy-duty bags are widely used for raw material circulation. For high-value materials sensitive to humidity and light, ordinary single-layer packaging cannot meet protection requirements. As high-end packaging products made of multi-layer composite materials, aluminum-plastic heavy-duty bags strike a balanced performance among strength, barrier property and sealing through structural design. Centered on aluminum-plastic heavy-duty bags, Xingchen Group has built a complete technical system covering material selection and manufacturing processes.
I. Material Composition of Aluminum-Plastic Heavy-Duty Bags
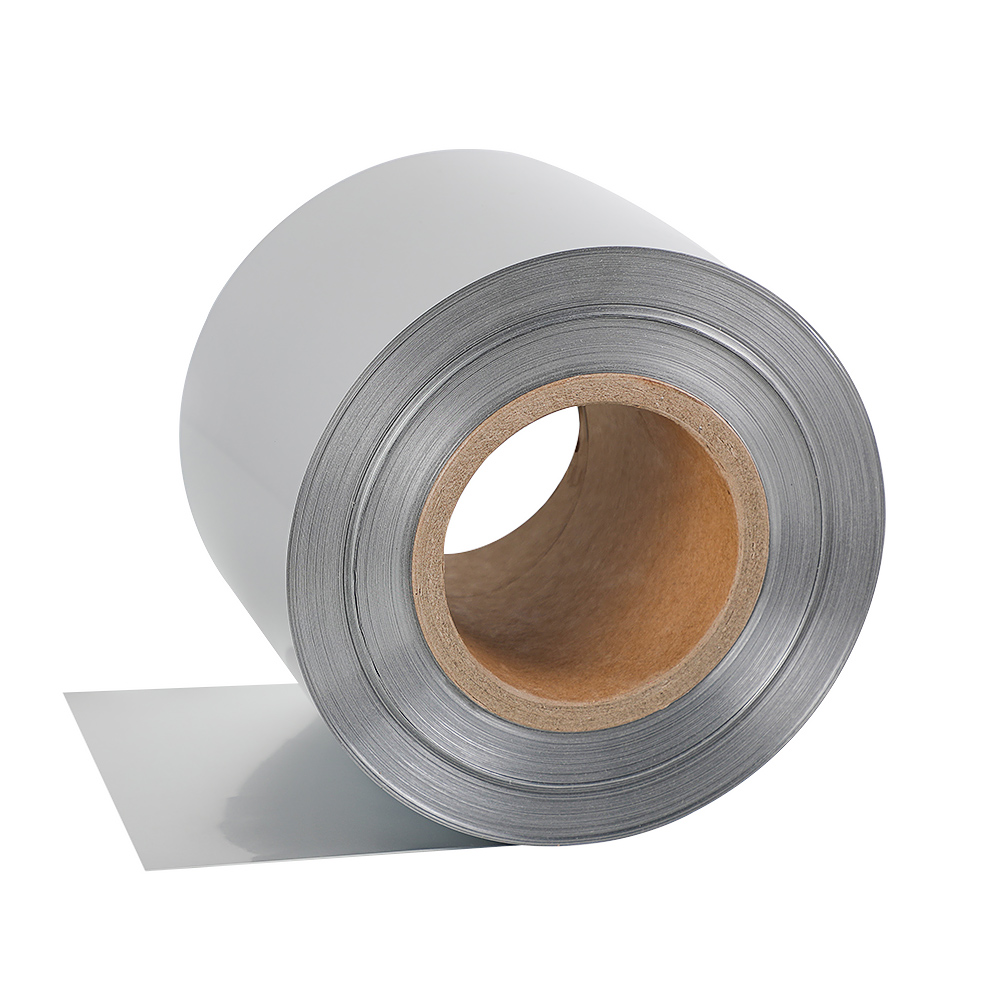
Aluminum-plastic heavy-duty bags are high-end packaging materials laminated with a multi-layer structure (PET+AL+NY+PE) with excellent performance and wide applicability. The PET layer delivers structural strength and printability; the AL aluminum foil layer provides barrier protection; the NY nylon layer improves puncture resistance and tensile strength; the PE layer is responsible for heat sealing. The four layers perform their respective functions, forming a packaging system with both load-bearing capacity and protective performance.
II. Dual Advantages of Strength and Barrier Performance
Aluminum-plastic heavy-duty bags feature two core strengths. In terms of mechanical performance, the outer layer offers favorable strength and wear resistance, while the inner layer boasts outstanding heat sealing and sealing performance. For barrier performance, the aluminum foil layer effectively blocks air, water vapor and light to prevent oxidation, moisture absorption and deterioration of packaged contents. The combination of these two strengths makes the bags suitable for application scenarios with stringent packaging standards.
III. Industry Coverage
Aluminum-plastic heavy-duty bags are widely adopted in pharmaceutical, chemical, electronic and food industries, especially for high-value products with strict packaging requirements. In addition, Xingchen’s 25kg aluminum foil heavy-duty bags have tailored solutions for functional materials including special engineering plastics, cable modified plastics, plastic alloy modified pellets, modified nylon, elastomer modified plastics, biodegradable modified plastics and flame-retardant modified plastics, satisfying demands for moisture resistance, oxygen barrier, light shielding and dust prevention.
IV. Process Assurance from FFS Heavy-Duty Bag Production Lines
Xingchen FFS heavy-duty bags mainly refer to aluminum-plastic heavy-duty bags. They feature light shielding to prevent photodegradation, moisture and water resistance, airtightness against oxidation, as well as puncture and breakage resistance, with a load range of 20–50 kg. They are widely used for resin pellets, TPE synthetic rubber, biodegradable pellets, PBAT pellets, lithium battery materials, metal powders and other materials. The FFS heavy-duty bag workshop adopts high-standard aluminum-plastic film production lines. Each production line upholds rigorous quality standards to guarantee consistent product quality, supported by certifications including ISO9001, SGS, RoHS and REACH.
V. Inspection and Quality Control System
Finished products undergo comprehensive and strict quality inspections covering appearance, seal integrity, seal strength, leakage and pinhole detection, compressive strength, puncture resistance, bond strength and other indicators. Full-process quality supervision ensures reliable quality. For heavy-duty bags, seal strength and leakage tests are particularly critical, as they directly determine sealing stability during transportation and stacking.
VI. Production Capacity and R&D Support
Xingchen is equipped with advanced manufacturing technology and multiple high-standard heavy-duty bag production lines, supporting a stable monthly output of 900,000 bags. The group prioritizes R&D and innovation as one of its core strategic objectives. It invests 6% of annual turnover in R&D, and continuously develops new products via its technology platform to maintain product innovation and long-term competitiveness.
Conclusion
Every technical link of aluminum-plastic heavy-duty bags, from material composition to process control, is developed to match the practical demands of high-end industrial packaging. With over two decades of experience in custom industrial packaging, Xingchen delivers stable and reliable heavy-duty packaging solutions for customers in pharmaceutical, chemical, electronic and other industries.