How to Select 25KG Heavy-Duty Bags: A Packaging Decision Framework Based on Material Characteristics
In industries including chemical, building material and food additive sectors, a broken 25kg raw material package may lead to product losses worth thousands of yuan, transportation disputes and even customer trust crises. Statistics show that up to 30% of customer complaints stem from packaging leakage, moisture ingress or insufficient load-bearing capacity. As a source manufacturer with over 20 years of expertise in industrial packaging, Xingchen Packaging is committed to delivering high-quality and diversified packaging solutions, guiding customers to make proper selection decisions based on material properties.
I. Select Materials by Protection Grade
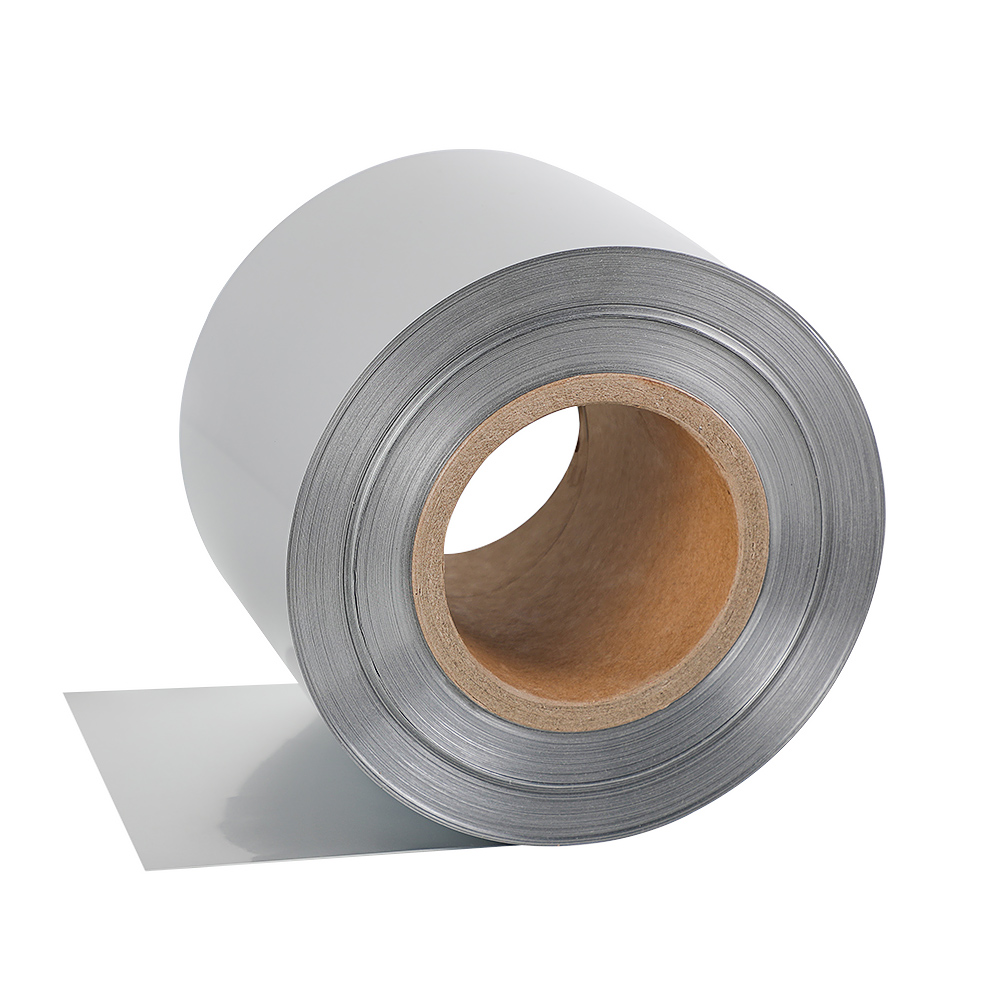
Protection requirements vary greatly among different materials. For high-value products requiring high-barrier protection, aluminum-plastic heavy-duty bags are premium packaging materials laminated with multi-layer structures (PET+AL+NY+PE) and deliver outstanding performance. High mechanical strength comes from the outer layer with good strength and wear resistance, together with the inner layer featuring excellent heat sealing and sealing performance. Its superior barrier property is achieved by the aluminum foil layer, which effectively blocks air, water vapor and light to prevent oxidation, moisture absorption and deterioration of contents. Widely used in pharmaceutical, chemical, electronic and food industries, it is especially suitable for high-value products with stringent packaging standards.
II. Select Bag Type by Filling Method
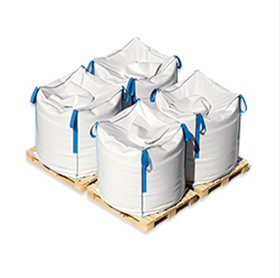
For automated filling scenarios, PE valve bags adopt a special design. Materials are filled through a valve at the top or bottom to realize dust-free automatic filling. Featuring good standing stability, the bags maintain their shape after filling for easy stacking and storage. They are highly compatible with various filling equipment to boost packaging efficiency. Primarily used for export business, they serve chemical, food and building material industries, and are ideal for dusty materials such as cement and flour.
III. Select Solutions by Temperature Control Requirements
For high-temperature filling applications, Xingchen Group’s technical team has developed high-temperature resistant heavy-duty bag solutions. Temperature tolerance can be customized: options cover 80℃–130℃ high-temperature resistance or low-temperature suitability ranging from -50℃ to -20℃. The three-layer composite structure (tensile and heat-resistant outer layer + barrier middle layer + heat-resistant inner layer) guarantees strength and sealing performance under high temperatures. Custom 4-layer, 5-layer and 6-layer composite structures are available for special demands such as enhanced barrier performance, puncture resistance and temperature tolerance. This solution enables direct filling on customers’ production lines, greatly improving production efficiency and cutting operating costs.
IV. Cost-Effective Option for Basic Protection
For routine moisture and water resistance needs, PE heavy-duty bags are made of premium polyethylene (PE). Transparent, anti-slip and stackable, they are cost-effective large packaging bags suitable for manual or semi-automatic filling. Their moistureproof and waterproof performance blocks water intrusion to keep packaged goods dry and safe, while tensile and wear-resistant properties preserve packaging integrity and durability. They are applicable to bulk materials such as chemical raw materials, plastic pellets, food additives and agricultural fertilizers.
V. Production Capacity & Quality Control Assurance
Equipped with advanced manufacturing technology and multiple high-standard heavy-duty bag production lines, Xingchen Packaging maintains a stable monthly output of 900,000 bags. Every detail is subject to rigorous quality inspection covering appearance, seal integrity, seal strength, leakage and pinhole detection, compressive strength, puncture resistance, bond strength and more, with strict quality oversight throughout the whole workflow.
Conclusion
Packaging selection is not merely picking a product, but matching material characteristics, filling methods, storage and transportation conditions with packaging structures. Drawing on 20 years of industry experience, Xingchen Packaging has helped hundreds of enterprises tackle packaging challenges.